Dirty Water and Mill Scale
Casting, rolling and quenching loops can carry scale, iron oxide, oil and suspended solids.
Steel and metallurgical plants require cooling systems that can handle high heat load, heavy dust, scale-laden water,
continuous operation and demanding equipment protection. Cooling towers, closed circuit cooling towers, dry coolers,
heat exchangers, filtration systems and pump stations must be selected around the actual process, water quality and reliability target.
This page explains how steel and metallurgy cooling systems work, how to separate clean and dirty cooling water loops,
how to choose between open cooling towers, closed circuit cooling towers, dry coolers and hybrid systems,
and what engineering data is needed for furnaces, continuous casting machines, rolling mills, induction heating systems,
hydraulic equipment and metallurgical utility cooling loops.
Steel and metallurgy cooling is directly connected to production uptime, equipment life, product quality and plant safety.
Cooling systems may serve electric arc furnaces, induction furnaces, continuous casters, rolling mills, mold cooling,
roll cooling, hydraulic oil systems, power electronics, transformers, compressors and central utility water systems.
Unlike standard HVAC cooling, metallurgical cooling often involves high heat flux, dirty water, iron oxide scale,
dust, oil contamination, high ambient temperature, corrosion risk and continuous-duty production.
A professional solution should define the cooling loop type first: clean loop, dirty loop, direct contact loop,
indirect heat exchanger loop or closed circuit cooling loop.
Steel plants create some of the hardest cooling water conditions: heat, scale, suspended solids and continuous-duty equipment.
Casting, rolling and quenching loops can carry scale, iron oxide, oil and suspended solids.
Induction coils, furnace jackets and hydraulic systems should not be treated like dirty spray water loops.
Scale and sediment can plug spray nozzles, strainers and heat exchangers.
Radiant heat, dust and continuous operation require robust materials and easy maintenance access.
Steel and metallurgy cooling must handle high heat, dirty water, scale, oil, dust and continuous production. The first decision is often how to separate dirty spray water from clean equipment protection loops.
Thermocore products are selected by water loop: open cooling towers with filtration for dirty high-flow loops, closed circuit towers for induction coils, furnace jackets and hydraulic systems, dry coolers for closed auxiliary loops, and heat exchangers to separate clean and dirty water.
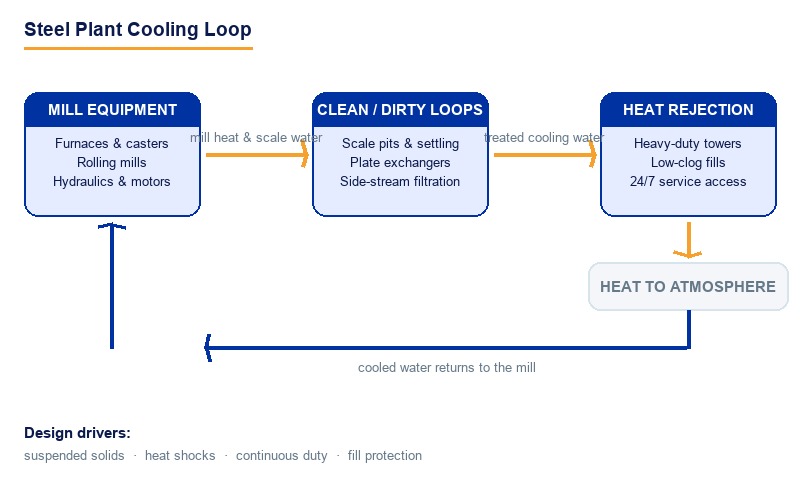
Steel plant cooling is organized by water cleanliness. Thermocore equipment helps reject heat from dirty loops, protect clean loops and reduce fouling risk through loop separation, filtration and maintainable components.
Metallurgy cooling should be selected according to heat load, water cleanliness, solids content, temperature requirement,
operating continuity, water availability and maintenance capability.
Cost-effective evaporative cooling for large utility cooling water loops where water treatment, filtration and basin cleaning are managed.
Closed-loop evaporative cooling for clean water loops, induction furnace coils, hydraulic systems and sensitive equipment.
Closed-loop dry cooling for water-saving systems, glycol loops, hydraulic oil cooling and power electronics cooling.
Dry cooling with evaporative assistance for sites that need water savings with peak cooling support during hot conditions.
Steel cooling selection should start by separating dirty spray water from clean equipment protection loops.
| Industry Condition | Better-Fit Product | Why It Fits | Selection Caution |
|---|---|---|---|
| Dirty spray, quench or rolling mill water with treatment | Open Cooling Tower plus Filtration | Handles large heat loads when combined with sediment removal and water treatment. | Requires basin cleaning, filtration, drift control and fouling management. |
| Induction coil, furnace jacket or hydraulic clean loop | Closed Circuit Cooling Tower | Protects clean fluid from dirty plant environment and outdoor contamination. | Coil material, water quality and pressure drop must be reviewed. |
| High-temperature closed auxiliary loop or water-saving duty | Dry Cooler | Closed-loop low-water heat rejection for suitable temperature ranges. | Hot ambient conditions may require larger coils or backup cooling. |
| Dirty loop separated from sensitive equipment | Heat Exchanger plus Cooling Tower | Allows dirty plant water to be isolated from clean machine water. | Heat exchanger fouling and cleaning access must be designed in. |
The best cooling system depends on whether the loop is clean or dirty, whether the fluid can be exposed to air,
how much water can be used and what outlet temperature is required.
| Item | Open Cooling Tower | Closed Circuit Cooling Tower | Dry Cooler | Hybrid / Adiabatic Cooling |
|---|---|---|---|---|
| Cooling Principle | Direct evaporative cooling of circulating water | Closed fluid coil cooled by spray water and air | Finned coil rejects heat to ambient air | Dry cooling with wet or adiabatic assistance |
| Water Cleanliness | Water exposed to air; filtration/treatment needed | Process fluid protected inside coil | Process fluid protected inside finned coil | Depends on system configuration |
| Water Use | Evaporation and blowdown required | Spray water loop required | Very low water use in dry operation | Lower than full wet operation when dry mode is available |
| Best Fit | Large utility loops and dirty water systems with treatment | Clean loops, induction coils, hydraulic systems and power equipment | Water-saving clean loops, oil cooling and auxiliary systems | Sites needing water saving and peak performance support |
| Main Caution | Scale, sludge, suspended solids, basin cleaning and water treatment | Coil scaling, spray water treatment and access for cleaning | Limited by dry bulb temperature and larger heat exchange area | More complex mode control and water quality review |
These are the practical failure points to check before choosing between an open cooling tower, closed circuit cooling tower, dry cooler or evaporative condenser.
Mixing dirty and clean loops can damage coils, induction equipment and hydraulic systems.
Scale and sediment reduce cooling and create uneven temperature control.
Unsuitable materials wear quickly in hot, dirty and chemically treated water.
No isolation or redundancy can turn routine cleaning into a shutdown event.
One of the most important engineering decisions in steel plant cooling is loop separation. Clean loops protect sensitive equipment,
while dirty loops handle direct cooling water that may contain scale, solids and oil.
Clean loops are used when water quality must be controlled to protect equipment. They may be closed-loop systems or separated from dirty water
through plate heat exchangers or closed circuit cooling towers.
Dirty loops serve direct contact cooling, spray systems, roll cooling or quench water where scale and suspended solids are expected.
They require filtration, sediment removal and maintainable basins.
A strong metallurgy solution page should connect cooling equipment with the actual plant systems and heat sources that need protection.
Water-cooled induction coils, furnace panels, ducts and high-temperature equipment.
Clean, stable cooling for mold heat removal and casting process control.
Direct cooling water systems that often require filtration and scale management.
Roll cooling, bearing cooling, mill stand cooling and hydraulic support systems.
Cooling for hydraulic power units, presses, rolling mills and casting equipment.
Closed-loop cooling for induction power supplies, rectifiers, transformers and electrical equipment.
Plate or shell-and-tube exchangers separating clean and dirty water loops.
Pumps, strainers, filters, settling basins and water treatment equipment supporting cooling reliability.
Metallurgical cooling design must consider heat load, loop cleanliness, solids concentration, water quality,
operating continuity and maintenance strategy. A correct design protects equipment and reduces production interruption risk.
Metallurgy cooling selection should include both thermal data and water contamination data.
If exact heat load is not available, equipment power, water flow and temperature difference can support preliminary selection.
| Required Data | Why It Matters |
|---|---|
| Process Type | Furnace, caster, rolling mill, quench system or auxiliary cooling affects equipment selection. |
| Equipment Served | Defines whether the loop is sensitive clean cooling or dirty direct contact cooling. |
| Heat Load / Cooling Capacity | Defines total heat rejection duty. |
| Water or Fluid Flow Rate | Determines pump flow, pipe size, tower loading and pressure drop. |
| Inlet Water or Fluid Temperature | Defines hot-side condition entering the cooling equipment. |
| Outlet Water or Fluid Temperature | Defines required cooling target and approach. |
| Clean Loop or Dirty Loop Requirement | Determines open/closed design, filtration and heat exchanger separation. |
| Water Quality and Suspended Solids | Affects scale control, filtration, material selection and maintenance frequency. |
| Oil Contamination or Scale Risk | Important for dirty water loops, rolling mill water and direct cooling systems. |
| Wet Bulb or Dry Bulb Design Data | Required for evaporative cooling tower or dry cooler selection. |
| Operating Hours, Redundancy and Footprint | Determines maintainability, standby capacity, tower cell count and plant layout. |
Steel plant cooling water often carries scale, dust, oil and suspended solids. Heat rejection equipment alone cannot solve dirty water problems.
Filtration and sediment management must be designed together with the cooling tower system.
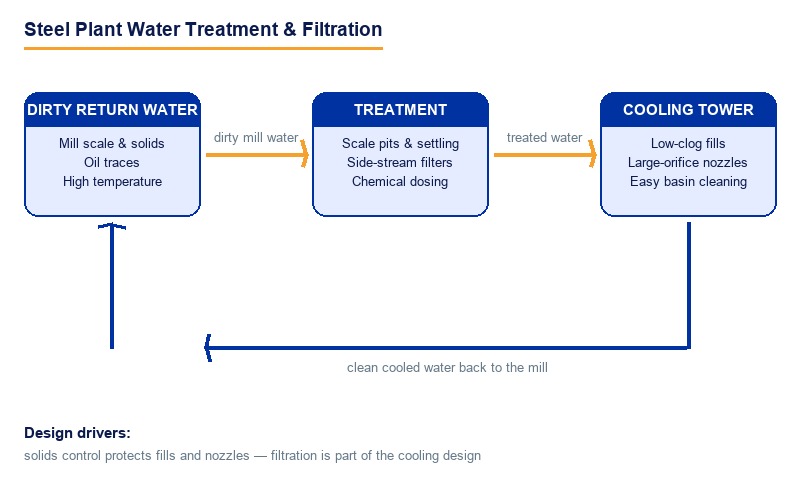
Heavy iron oxide scale should be separated before water reaches pumps, nozzles, heat exchangers or cooling towers.
Filters, strainers or magnetic separation can reduce suspended solids and protect heat transfer surfaces.
Heat exchangers or closed-loop systems help prevent dirty process water from entering sensitive equipment circuits.
Water quality directly affects cooling tower performance, heat exchanger cleanliness, pump reliability and equipment life.
Metallurgical plants should evaluate both chemical water quality and physical contamination.
Scale, dust and sludge can block spray nozzles, foul fill, clog heat exchangers and increase pump wear.
Hardness, conductivity, pH, chlorides and oxygen can create scale or corrosion in towers, coils and piping.
Rolling mill and hydraulic systems may introduce oil, grease or process contaminants into water loops.
Maintenance should focus on scale removal, filtration, water treatment, heat transfer cleanliness and mechanical reliability.
A maintainable system reduces shutdown risk and protects critical production equipment.
Basins, nozzles, fill, strainers and drift eliminators should be inspected and cleaned to control sludge and fouling.
Filters, heat exchangers and settling systems should be cleaned based on pressure drop, solids load and process duty.
Pumps, fans, motors, VFDs, valves, temperature sensors and flow instruments should be checked regularly.
Steel and metallurgy cooling systems can be customized according to process type, heat load, water contamination,
clean/dirty loop separation, filtration, material requirements, redundancy, site layout and maintenance strategy.
Designed around furnace, caster, rolling mill, hydraulic system, heat exchanger or auxiliary cooling duty.
Configured for clean loop, dirty loop, direct cooling, indirect heat exchanger separation, filtration and sediment removal.
Adjusted for standby pumps, multi-cell towers, modular expansion, service access, control alarms and heavy-duty operation.
Send your process type, equipment served, heat load, water flow rate, inlet and outlet temperature,
clean or dirty loop requirement, water quality, suspended solids, oil contamination risk, dust condition,
wet bulb or dry bulb design data and footprint.
Our engineering team will review whether an open cooling tower, closed circuit cooling tower, dry cooler,
hybrid system or heat exchanger-separated loop is more suitable.
These FAQs are written for steel plant engineers, metallurgy equipment suppliers, EPC contractors, foundries,
rolling mill operators and industrial buyers who need to understand furnace cooling, casting cooling,
rolling mill cooling, clean and dirty water loops, cooling tower selection, filtration, water quality,
maintenance and quotation data.
A steel and metallurgy cooling solution is a heat rejection system designed to remove heat from furnaces, continuous casting machines, rolling mills, induction heating systems, hydraulic systems, quench systems, heat exchangers, power electronics and plant utility cooling water loops. It may include open cooling towers, closed circuit cooling towers, dry coolers, adiabatic coolers, heat exchangers, filtration, sediment removal, pumps, controls and water treatment.
Heat from steelmaking or metallurgical equipment is transferred into direct cooling water, indirect closed-loop cooling water, glycol loops, hydraulic oil coolers or heat exchangers. The warm water or fluid is then sent to a cooling tower, closed circuit tower, dry cooler, adiabatic cooler or central cooling water system. Heat is rejected to outdoor air, and the cooled fluid returns to the furnace, caster, mill, mold, hydraulic system or auxiliary equipment.
Clean loop cooling usually serves sensitive equipment such as furnace coils, power supplies, hydraulic oil coolers, caster molds, heat exchangers or closed circuits where water quality must remain controlled. Dirty loop cooling may serve direct contact cooling, scale-laden water, sprays, roll cooling or quench systems where water can contain iron oxide scale, suspended solids, oil or process contamination. These loops should normally be separated by heat exchangers, filtration or dedicated cooling systems.
There is no single best type for all steel and metallurgy applications. Open cooling towers are commonly used for large utility cooling water systems where water quality can be managed. Closed circuit cooling towers are useful for clean loops, induction furnaces, power electronics and sensitive equipment. Dry coolers are suitable for water-saving closed loops and auxiliary cooling. Adiabatic or hybrid systems may be used when water saving and peak cooling performance must be balanced.
A closed circuit cooling tower is suitable when the cooling fluid must remain clean and protected from dust, scale, oxygen and outdoor contamination. It is commonly used for induction furnace coils, power supply cooling, hydraulic systems, water-cooled electrical equipment, clean utility loops, glycol systems and heat exchangers serving critical metallurgical equipment.
A dry cooler is suitable when water saving, closed-loop operation, lower water treatment complexity or reduced plume is important, and when the required outlet temperature can be achieved above ambient dry bulb temperature. Dry coolers are often used for hydraulic oil cooling, glycol loops, power electronics, transformer support, auxiliary equipment and clean water circuits in suitable climates.
Water quality affects scaling, corrosion, biological growth, suspended solids, oil contamination, nozzle blockage, fill selection, coil material and maintenance frequency. High solids or scale-laden water may require open towers with filtration and basin cleaning, while sensitive clean loops may require heat exchanger separation, closed circuit cooling or dry cooling.
Important data includes equipment served, heat load, water or fluid flow rate, inlet and outlet temperature, water quality, suspended solids level, oil contamination risk, process type, clean or dirty loop requirement, design wet bulb or dry bulb temperature, project location, operating hours, redundancy requirement, footprint, dust level, corrosion environment, noise requirement and material preference.
Common options include FRP casing, galvanized steel, stainless steel 304 or 316, aluminum-zinc coated panels, heavy-duty steel structures, PVC or PP fill, corrosion-resistant nozzles, drift eliminators, carbon steel coils, stainless steel coils, coated coils, axial fans and robust hardware. Material selection depends on water quality, ambient dust, corrosion environment, temperature and expected service life.
To request a quotation, send the process type, equipment served, heat load, water or fluid flow rate, inlet and outlet temperature, design wet bulb or dry bulb temperature, project location, clean or dirty loop requirement, water quality, suspended solids, oil contamination risk, operating hours, redundancy requirement, footprint, dust and corrosion conditions, power supply and material preference.
Send us your process type, equipment served, heat load, water or fluid flow rate, inlet and outlet temperature,
design wet bulb or dry bulb temperature, project location, clean or dirty loop requirement, water quality,
suspended solids, oil contamination risk, operating hours, redundancy requirement, footprint, dust and corrosion conditions,
power supply and material preference. We will help you evaluate the right steel and metallurgy cooling solution.